Overview
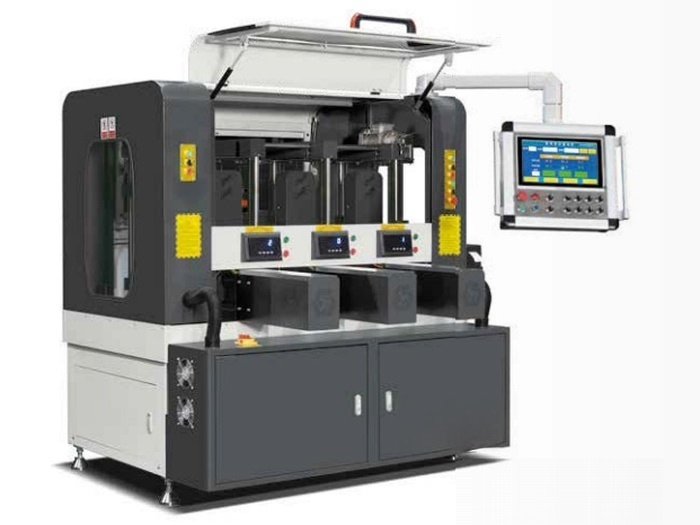
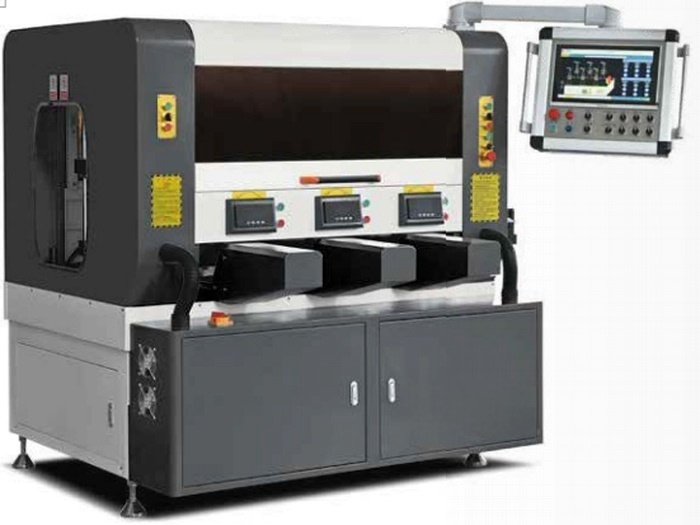
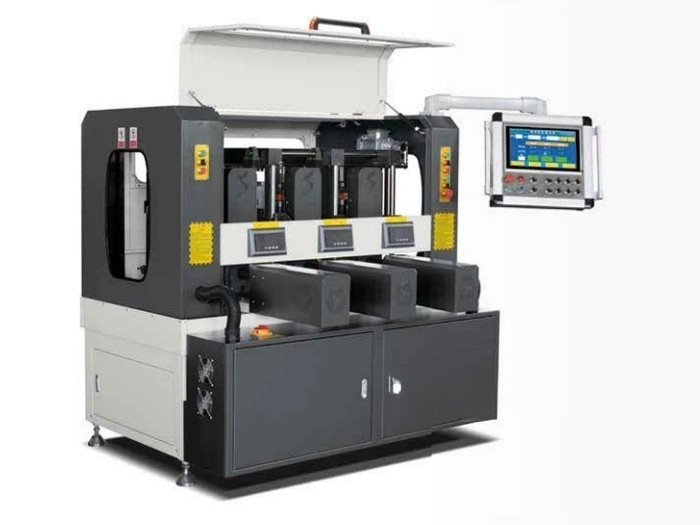
The TFH-11CNC is an 11-axis CNC rolling & crimping machine for thermal-break aluminium profiles. After knurling and PA66 strip insertion, the profile and the insulating strip are permanently locked together by precision rolling — the step that decides the shear strength, thermal performance and long-term stability of the finished thermal break profile.
Six groups of cutter heads, the nylon pressure rollers and three pressure groups are all positioned by CNC. More than 2,000 aluminium profile programs are stored in the control system, so a change of profile is a one-button recall instead of half an hour of manual re-adjustment. Precision guide rails, precision ball screws, Schneider electrical components and stepless frequency-converter speed control keep batch after batch consistent.
Key Features
- 11-axis CNC adjustment — six cutter-head groups, nylon rollers and three pressure groups positioned numerically for repeatable, batch-consistent crimping.
- One-button changeover — more than 2,000 aluminium profile programs stored in memory; recall saved parameters instead of re-adjusting by hand.
- Free strip-width adaptation — the upper and lower width of each upper cutter head is CNC-adjustable, so different strip widths run without changing tooling.
- Built-in straightening — nylon cots move up and down to straighten bowed profiles and hold verticality and parallelism after pressing.
- Misalignment ready — the rear separation lower cutter head (3 segments) is manually adjustable for profiles with staggered grooves.
- Industrial-grade hardware — precision guide rails, precision ball screws, Schneider electrics, servo pressure control and stepless speed regulation.
Technical Specifications
| Parameter | Value |
|---|---|
| Power supply | 380 V / 50 Hz |
| Total power | 11.5 kW |
| CNC axes | 11-axis CNC |
| Cutter-head separation distance | 0–180 mm |
| Cutter-head opening height | 8–90 mm |
| Max. profile cross-section | 300 × 300 mm |
| Positioning accuracy | ± 0.05 mm |
| Profile feeding speed | 6–60 m/min |
| Overall dimension | 1700 × 1550 × 1850 mm |
| Machine weight | ≈ 1,610 kg |
| Profile program memory | 2,000+ profiles, one-button recall |
| ERP machine option | Available on request |
Working Process
- Feeding — the knurled and strip-inserted profile enters the rolling station on the infeed conveyor.
- Positioning — the stored program recalls the 11 axis positions: six cutter-head groups, the nylon cots and the three pressure groups all move to the values saved for this profile. On profiles with staggered grooves the three-segment rear separation lower head is trimmed by hand — the only manual touch on the machine.
- Rolling & crimping — the cutter heads press the groove walls over the PA66 strip to the crimp value held in the program. Any single pressure group can be trimmed without losing the stored baseline.
- Output — finished profiles leave straight and parallel, ready for packing, machining or the thermal break assembly line.
Quality & Standards
Every TFH machine is assembled and inspected above industry standard with a three-step pre-delivery inspection. On the 11-axis model that includes an eight-hour batch on a standard window profile, with crimp depth and straightness checked at the start, middle and end of the run — profiles must not de-strip. Rolled sections hold longitudinal shear to GB/T 5237.6-2017 and bending to the high-precision class of GB/T 5237.1-2017.
Applications
- Aluminium window and door plants crimping standard thermal-break sections in high volume, where one groove height covers most of the catalogue.
- Workshops moving from manual crimping to CNC: 2,000+ stored programs replace roughly half an hour of hand adjustment for every profile change.
- Plants that also meet occasional staggered-groove work — the three-segment rear lower head covers it without a second machine.
Part of the TFH rolling & crimping range — five models from 11 to 37 axes. If more than a few of your profiles sit higher on one side, the TFH-14CNC adds 3-axis CNC lifting and removes that manual step.
FAQ
Which profiles can the TFH-11CNC handle?
Standard thermal-break window, door and facade sections with a single groove height, up to a 300 × 300 mm cross-section. It is the right starting point when your catalogue contains no high/low-groove or double-offset profiles.
How long does a profile changeover take?
One button. Six cutter-head groups, the nylon cots and three pressure groups move to the stored values; only the three-segment rear lower head needs a manual check on staggered grooves. Most plants are running again in minutes, against roughly half an hour on a manual machine.
Do different strip widths need different tooling?
No. The upper and lower width of each cutter head is CNC-adjustable, so different strip widths within the 80–100 mm range run without changing cutters.