Overview
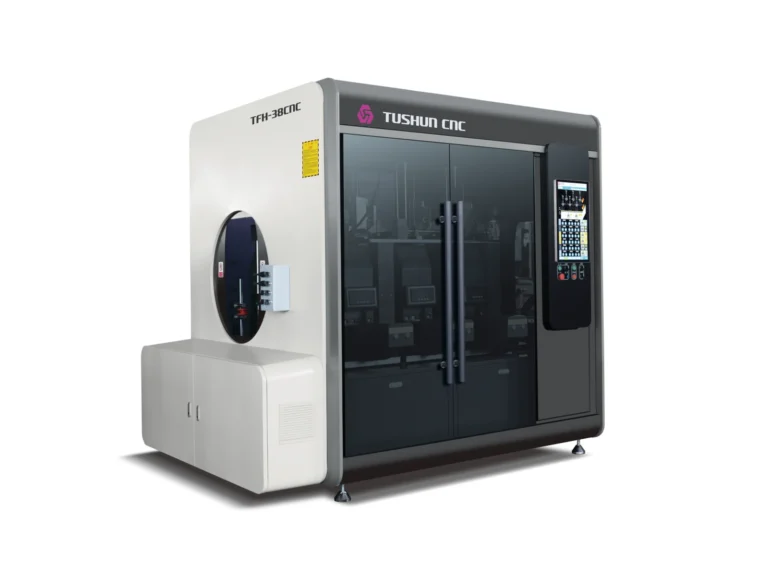
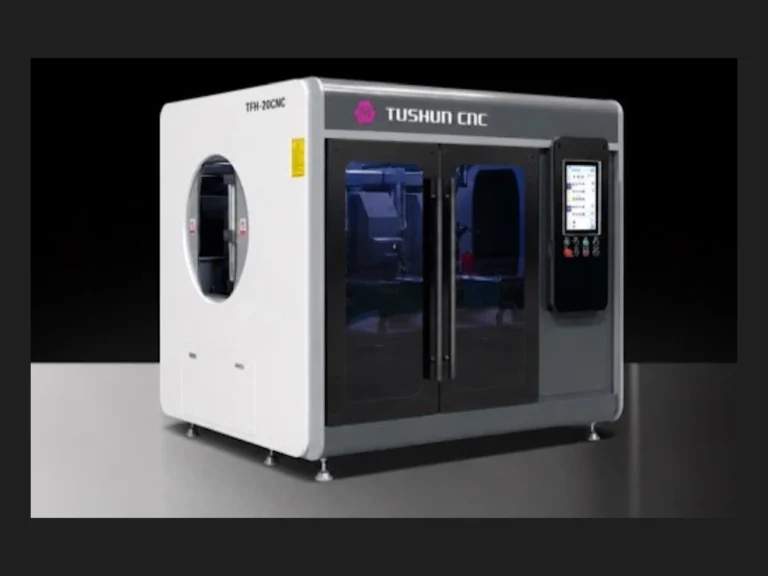
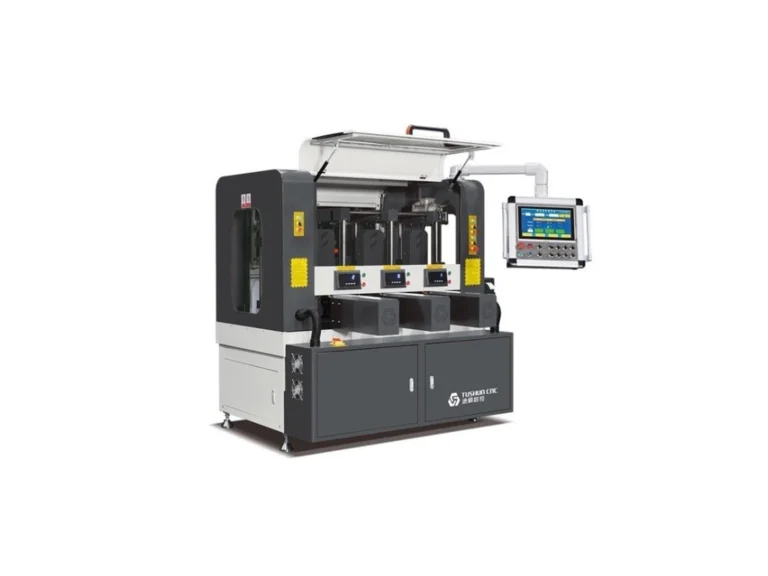
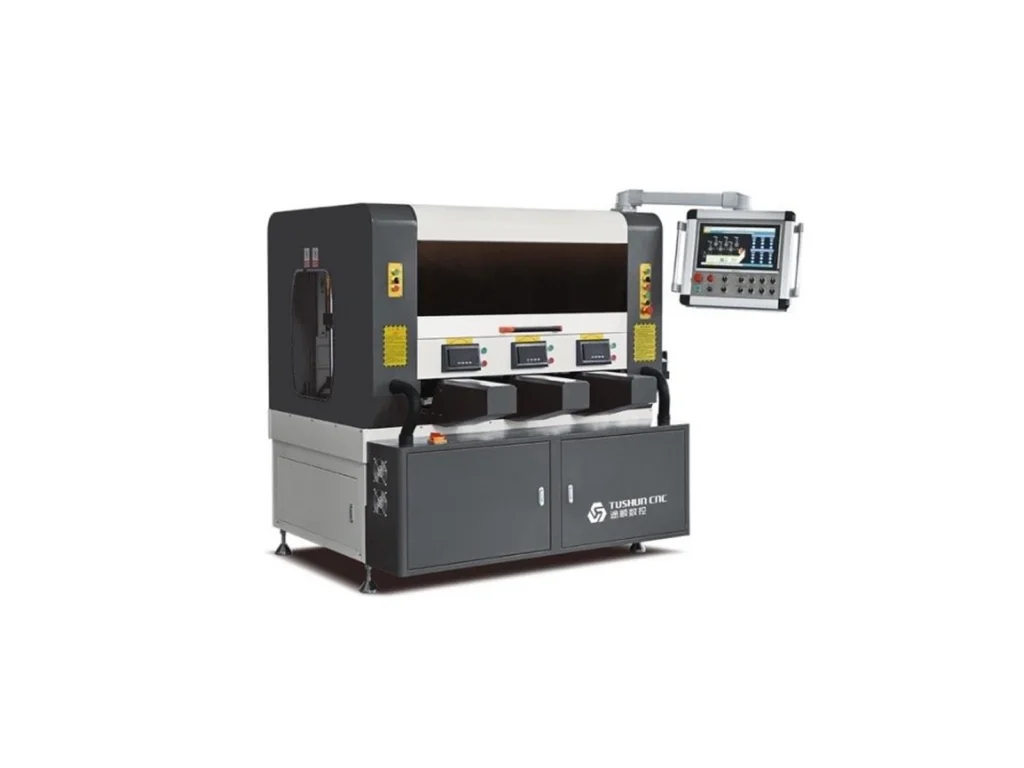
The TFH-17CNC handles compound misalignment in both directions: the front separation upper cutter heads (3 segments) translate forward and backward while the rear separation lower cutter head lifts up and down. Profiles whose strip and groove are offset on both axes — typical of shaped window and curtain-wall sections — come out crimped in a single pass.
Six cutter-head groups are numerically adjusted for 80–100 mm strips, 17 axes support quick changeover, and more than 2,000 profile programs are stored for one-button recall. The machine can be ordered as an ERP model for data interconnection with factory systems.
Key Features
- Two-direction misalignment — front separation upper cutter heads translate forward/backward; rear separation lower cutter head lifts up/down.
- Six CNC cutter-head groups for 80–100 mm strips, with CNC lifting nylon cots and three CNC pressure groups.
- Fast changeover — 17-axis CNC and 2,000+ stored aluminium profile programs with one-button positioning.
- Free strip-width adaptation — cutter-head width adjusts without tooling changes.
- Profile straightening — nylon cots raise and lower to correct bending quickly.
- ERP machine option — configurable for ERP integration on request.
Technical Specifications
| Parameter | Value |
|---|---|
| Power supply | 380 V / 50 Hz |
| Total power | 13.5 kW |
| CNC axes | 17-axis CNC |
| Cutter-head separation distance | 0–180 mm |
| Cutter-head opening height | 8–90 mm |
| Max. profile cross-section | 300 × 300 mm |
| Positioning accuracy | ± 0.05 mm |
| Profile feeding speed | 6–60 m/min |
| Overall dimension | 1700 × 1550 × 1850 mm |
| Machine weight | ≈ 1,838 kg |
| Profile program memory | 2,000+ profiles, one-button recall |
| ERP machine option | Available on request |
Profile Misalignment States
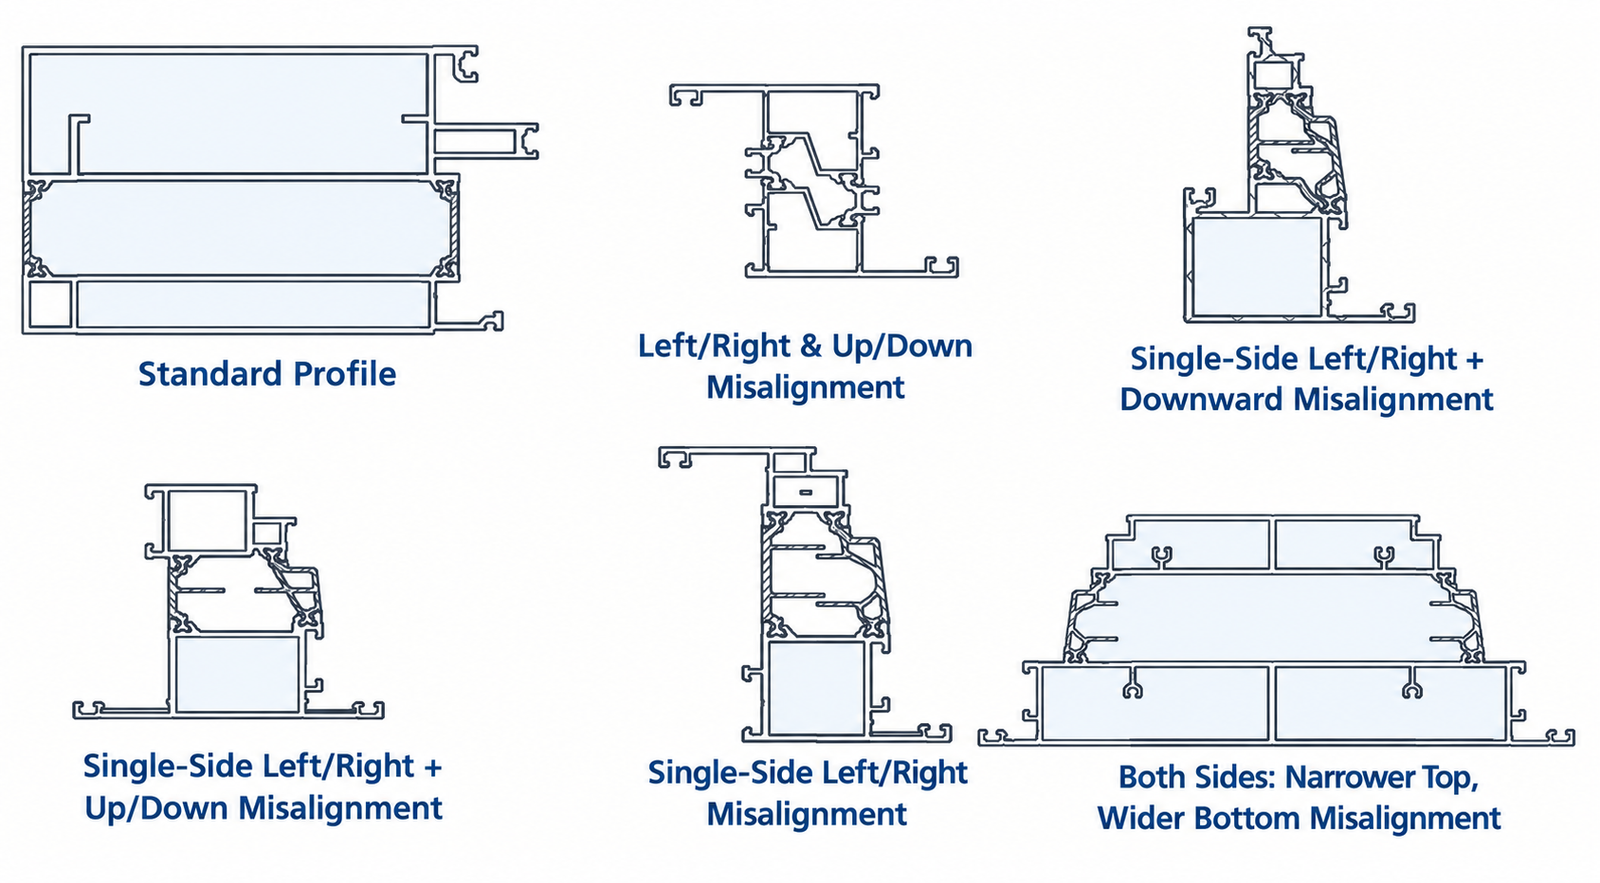
The 17-axis configuration adds profile misalignment and synchronized profile + strip misalignment to the up/down states.
Working Process
- Feeding — the knurled and strip-inserted profile enters the rolling station on the infeed conveyor.
- Positioning — stops, presses and pushers center the A-side profile, insulating strip and B-side profile for precise alignment.
- Rolling & crimping — servo-driven cutter heads press the groove walls over the strip to the standard crimp value.
- Output — finished profiles leave straight and parallel, ready for packing or machining.
Quality & Standards
Every TFH machine is assembled and inspected above industry standard with a three-step pre-delivery inspection. Rolled profiles hold longitudinal shear force to GB/T 5237.6-2017 and bending to the high-precision class of GB/T 5237.1-2017, with high batch consistency and a low defective rate.
Applications
- Aluminium window and door profile plants crimping misaligned and standard thermal-break sections in mixed series.
- Curtain-wall and facade profile lines with shaped sections and staggered strip grooves.
- Factories that need repeatable changeover between many profile programs on one machine.
FAQ
Which axis configuration do I need?
It depends on the misalignment states of your profile cross-sections. Standard profiles run on the 11-axis machine; up/down and compound misalignment needs 14–37 axes. Send us your profile drawings and we will confirm the right configuration.
How fast can we change profiles?
More than 2,000 profile programs are stored. Recall the saved program and the machine positions itself — no manual re-adjustment of cutter heads or pressure.
Do different strip widths need different tooling?
No. The upper and lower width of each cutter head is adjustable, so the machine runs different strip widths without changing cutters.